Lightweight construction is an important consideration in modern boat and yacht manufacturing. Shipbuilders must balance structural strength, vessel weight, durability, interior comfort, and production costs while selecting materials for different components.
Traditional materials such as plywood, solid wood, and certain metal panels remain widely used in marine construction. However, these materials may increase structural weight or require additional protection against moisture, corrosion, or environmental degradation.
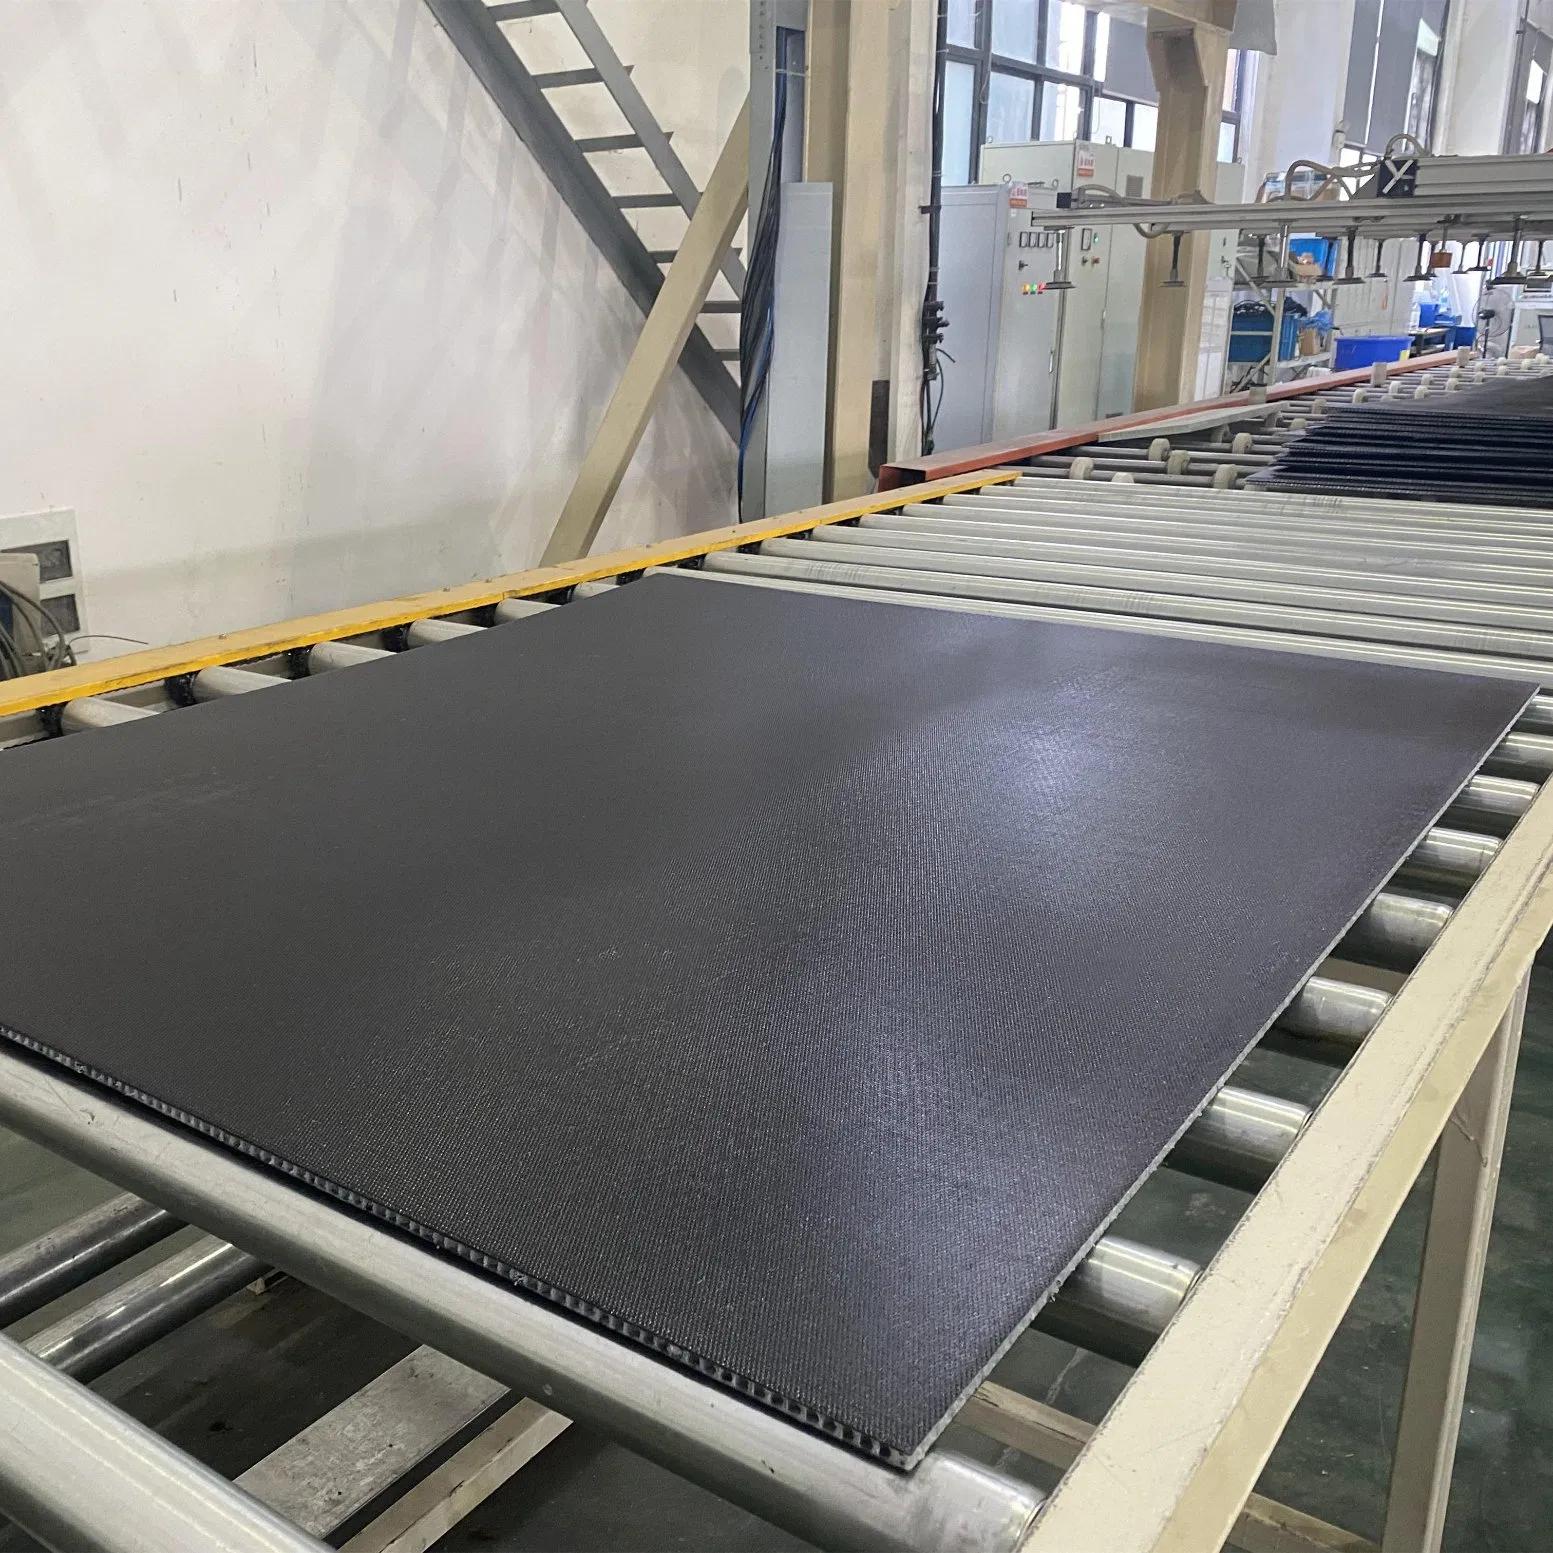
PP Honeycomb Panels offer an alternative approach to lightweight composite construction by combining a polypropylene honeycomb core with suitable face sheets. The resulting sandwich structure can provide useful stiffness and strength at a relatively low weight when properly designed and manufactured.
These panels can be considered for yacht furniture, cabin partitions, interior wall panels, lightweight access doors, and selected flooring applications. Depending on the design, face sheets may consist of fiberglass-reinforced plastic (FRP), compatible thermoplastic composites, aluminum, or other suitable materials.
Nevertheless, not every PP honeycomb panel is suitable for every marine application. Deck structures, load-bearing components, watertight bulkheads, and fire-rated interior systems require specific engineering validation.
This article examines how PP honeycomb panels contribute to lightweight boat and yacht construction, including their structure, material properties, typical parameters, manufacturing methods, and purchasing considerations.
2. What Is a PP Honeycomb Panel?
A PP Honeycomb Panel is a composite sandwich panel that uses a polypropylene honeycomb core between two outer face sheets.
The honeycomb core contains interconnected cellular structures that reduce the amount of solid material required to fill the panel’s internal volume.
The face sheets provide much of the panel’s tensile and compressive bending resistance, while the core maintains separation between the face sheets and transfers shear loads.
When the materials are correctly selected and bonded, this configuration can achieve a favorable stiffness-to-weight ratio.
2.1 Basic Panel Structure
A typical FRP-faced PP honeycomb sandwich panel consists of three main layers.
Top face sheet
The upper surface provides a finished appearance and contributes to the panel’s structural performance. FRP skins may offer corrosion resistance and design flexibility.
PP honeycomb core
The core reduces panel weight while supporting the face sheets. Its thickness, cell geometry, density, and shear properties influence the behavior of the complete panel.
Bottom face sheet
The lower surface completes the sandwich structure and contributes to its bending resistance and dimensional stability.
The adhesive interface between these layers is critical. Poor bonding can prevent the panel from achieving its intended structural performance, even when the individual materials have suitable properties.
2.2 Common Panel Configurations
| Panel Configuration | Typical Application | Key Consideration |
|---|---|---|
| FRP + PP Honeycomb Core + FRP | Boat interior panels and selected marine structures | Skin strength, core shear performance, and bonding |
| Decorative Skin + PP Honeycomb Core + Decorative Skin | Yacht furniture and cabinet panels | Surface finish, edge reinforcement, and hardware attachment |
| Aluminum Sheet + PP Honeycomb Core + Aluminum Sheet | Selected lightweight marine panels | Thermal compatibility, bonding, and corrosion management at connections |
| Thermoplastic Composite Skin + PP Honeycomb Core + Thermoplastic Composite Skin | Selected lightweight composite components | Material compatibility and consolidation process |
These configurations are examples rather than universally interchangeable products. Each combination requires validation for its intended service conditions.
3. Why Lightweight Panels Matter in Boat and Yacht Construction
Reducing unnecessary weight can improve vessel design efficiency, but the benefits depend on where weight is removed and how the vessel is operated.
PP honeycomb panels provide a potential solution for reducing the mass of selected interior and secondary structural components.
3.1 Reducing Interior Component Weight
Yachts contain numerous partitions, cabinets, doors, storage compartments, and decorative panels.
Although each component may be relatively small, their combined mass can be significant.
Replacing suitable solid constructions with lightweight sandwich panels can reduce the weight of these components while maintaining the required stiffness and functionality.
Potential applications include:
- Cabin wall panels.
- Lightweight furniture doors.
- Storage compartment partitions.
- Interior access panels.
- Selected tabletops and cabinet structures.
- Decorative wall and ceiling panels.
The final weight reduction depends on the original construction, selected face sheets, core density, panel thickness, and reinforcement requirements.
3.2 Improving Structural Efficiency
The separation between the two face sheets is one of the main reasons sandwich panels can achieve high bending stiffness relative to their weight.
In a sandwich structure, the face sheets resist tensile and compressive stresses associated with bending, while the core helps maintain their separation and transfer shear loads.
Increasing the distance between the face sheets can significantly increase bending stiffness, provided the core and bonding interfaces can transfer the resulting loads.
However, panel thickness alone does not determine structural performance. Core shear strength, face-sheet properties, bonding quality, support conditions, and concentrated loads must also be considered.
3.3 Supporting Corrosion-Resistant Construction
Polypropylene is not susceptible to electrochemical corrosion in the same way as metallic materials.
This can be useful in marine environments where saltwater, humidity, and condensation affect material durability.
However, a PP honeycomb panel may still contain metallic fasteners, inserts, or face sheets. These components require appropriate material selection and protection against galvanic or environmental corrosion where relevant.
3.4 Providing Design Flexibility
PP honeycomb panels can be manufactured in different dimensions and configurations according to project requirements.
Depending on the supplier’s capabilities, manufacturers may specify:
- Core thickness.
- Cell size.
- Core density.
- Face-sheet material.
- Face-sheet thickness.
- Panel length and width.
- Surface finish.
- Edge reinforcement.
- Insert locations.
- Required mechanical performance.
This flexibility supports customized marine interior components and composite panel production.
4. Typical Technical Parameters of PP Honeycomb Panels
Technical parameters should be selected according to the intended application rather than taken from a single universal specification.
The following tables provide a framework for evaluating PP honeycomb panels.
4.1 Core Material Parameters
| Parameter | Example Specification Format | Engineering Importance |
|---|---|---|
| Core material | Polypropylene (PP) | Determines the core’s basic material characteristics |
| Core density | kg/m³ | Influences mass and mechanical properties |
| Cell size | mm | Affects geometry, bonding, and mechanical behavior |
| Core thickness | mm | Influences panel thickness and bending stiffness |
| Compressive strength | kPa or MPa | Indicates resistance to through-thickness compression |
| Shear strength | kPa or MPa | Indicates the core’s capacity to transfer shear loads |
| Shear modulus | MPa | Helps predict deformation under shear loading |
| Water absorption | % under a specified test method | Helps assess moisture-related behavior |
| Operating temperature | °C under specified conditions | Establishes relevant service-temperature limits |
| Dimensional tolerance | mm | Supports manufacturing consistency |
Important: Numerical values should be obtained from the selected manufacturer’s technical data sheet. Core properties can vary considerably with density, cell geometry, material formulation, and test method.
4.2 Finished Panel Parameters
| Parameter | Specification Unit | Why It Matters |
|---|---|---|
| Total panel thickness | mm | Influences stiffness, weight, and installation space |
| Panel length | mm | Determines component dimensions |
| Panel width | mm | Determines component dimensions |
| Face-sheet thickness | mm | Affects bending resistance, impact resistance, and surface durability |
| Face-sheet material | FRP, aluminum, or compatible composite | Determines surface and structural properties |
| Finished panel density | kg/m³ | Helps estimate panel mass |
| Areal weight | kg/m² | Supports weight budgeting and material comparison |
| Flexural strength | MPa | Helps evaluate resistance to bending failure |
| Flexural stiffness | N·m² or another defined test unit | Helps evaluate resistance to deflection |
| Bonding strength | Defined test method and unit | Helps assess interface integrity |
| Fire performance | Applicable classification and test standard | Important for regulated marine interiors |
When comparing suppliers, buyers should confirm whether the quoted parameters refer to the core material or the complete sandwich panel.
These are different products with different performance characteristics.
5. Example: Estimating the Weight of a Marine Sandwich Panel
One of the most useful ways to evaluate lightweight construction is to calculate the mass per square meter of a proposed panel.
The following example illustrates the calculation using hypothetical design values.
Assume a panel has:
- Two FRP face sheets, each 1.5 mm thick.
- A PP honeycomb core 20 mm thick.
- An assumed core density of 80 kg/m³.
- An assumed FRP density of 1,800 kg/m³.
These values are illustrative and do not represent a verified ONEBOND product specification.
5.1 Weight Calculation
The mass per square meter of each layer can be estimated using:
Areal mass = Material density × Layer thickness
Thickness must be expressed in meters when density is specified in kg/m³.
For the two FRP face sheets:
2 × 1,800 × 0.0015 = 5.4 kg/m²
For the PP honeycomb core:
80 × 0.020 = 1.6 kg/m²
The estimated combined mass of the face sheets and core is therefore:
5.4 + 1.6 = 7.0 kg/m²
5.2 Example Weight Budget
| Component | Thickness | Assumed Density | Estimated Mass |
|---|---|---|---|
| Upper FRP face sheet | 1.5 mm | 1,800 kg/m³ | 2.7 kg/m² |
| PP honeycomb core | 20 mm | 80 kg/m³ | 1.6 kg/m² |
| Lower FRP face sheet | 1.5 mm | 1,800 kg/m³ | 2.7 kg/m² |
| Combined material layers | 23 mm | — | 7.0 kg/m² |
This estimate excludes adhesive, edge reinforcements, inserts, coatings, fittings, and manufacturing waste.
The actual panel weight must be verified using the selected materials and finished-panel measurements.
5.3 Comparing Alternative Panel Designs
To compare a PP honeycomb panel with plywood or PVC foam sandwich construction, manufacturers should calculate the mass of each complete panel using equivalent dimensions and comparable functional requirements.
The comparison should include all structural layers and reinforcements.
A lighter panel is not necessarily a better solution if it fails to meet stiffness, impact resistance, fatigue, or fastening requirements.
6. PP Honeycomb Panel Applications in Boats and Yachts
Different marine components have different structural requirements. PP honeycomb panels should therefore be selected according to their specific function.
6.1 Yacht Interior Wall Panels
Interior wall panels are common candidates for lightweight sandwich construction.
Potential benefits include lower panel mass, dimensional flexibility, and compatibility with different decorative face materials.
For these panels, manufacturers should evaluate:
- Required stiffness.
- Surface appearance.
- Cleaning and maintenance requirements.
- Moisture exposure.
- Fire and smoke regulations.
- Attachment methods.
- Edge sealing.
6.2 Cabin Partitions
Cabin partitions divide interior spaces and may support furniture or attached equipment.
A PP honeycomb panel may be suitable when the design loads are modest and the panel is properly supported.
However, partitions intended to provide fire separation, watertight separation, or primary structural functions must meet the applicable requirements for those functions.
The use of a lightweight core alone does not establish regulatory compliance.
6.3 Yacht Furniture and Cabinet Panels
Furniture is another potential application for PP honeycomb sandwich construction.
Cabinet doors, decorative partitions, and selected tabletops can benefit from reduced weight.
The main engineering challenge is often local load transfer rather than the overall panel weight.
For example, hinges and handles apply concentrated forces at relatively small attachment areas. Designers may need solid inserts, reinforced edges, or specialized fastening systems to prevent local failure.
6.4 Boat Flooring and Deck Panels
Floor and deck applications require more careful structural evaluation.
Panels must withstand distributed loads, concentrated loads, repeated foot traffic, and potentially severe environmental exposure.
Important design factors include:
- Core shear strength.
- Face-sheet reinforcement.
- Panel span.
- Support spacing.
- Local compression.
- Impact resistance.
- Surface slip resistance.
- Water ingress protection.
- Fatigue performance.
For deck panels supporting machinery or heavy equipment, additional structural reinforcement may be necessary.
The final design should be validated under the relevant loading conditions.
6.5 Lightweight Access Doors and Equipment Covers
PP honeycomb panels can also be considered for access doors, removable covers, and selected equipment enclosures.
These applications may benefit from reduced weight and customized panel dimensions.
However, designers should verify stiffness, impact resistance, fastening strength, sealing requirements, and the temperature conditions near the equipment.
7. PP Honeycomb Panels vs. Plywood and PVC Foam Panels
Boat and yacht manufacturers may compare PP honeycomb panels with plywood panels and PVC foam sandwich panels.
Each construction has advantages and limitations.
| Comparison Factor | PP Honeycomb Panel | Plywood Panel | PVC Foam Sandwich Panel |
|---|---|---|---|
| Construction | Thermoplastic honeycomb core with face sheets | Layered wood veneers | Closed-cell foam core with face sheets |
| Weight | Depends on core and skin design | Depends on wood species and thickness | Depends on foam density and skin design |
| Moisture behavior | PP core has low water absorption; panel edges still require protection | Depends on plywood grade, adhesive, coatings, and edge sealing | Depends on foam grade, face sheets, and bonding |
| Bending stiffness | Depends on panel architecture | Depends on plywood thickness and grade | Depends on core thickness, density, and skins |
| Local fastening | May require inserts or reinforced areas | Can provide practical fastening options depending on construction | May require inserts or reinforced areas |
| Bonding | PP surface may require special preparation | Depends on adhesive and substrate | Depends on foam and adhesive compatibility |
| Fabrication | Requires compatible bonding and finishing methods | Uses established woodworking processes | Compatible with various composite panel processes |
| Typical evaluation focus | Core shear, skin bonding, edge design | Moisture protection, stiffness, and fastener performance | Foam shear, compression, resin compatibility, and bonding |
The best material depends on the component’s requirements and the manufacturer’s existing production capabilities.
A complete panel comparison should consider mass, stiffness, strength, environmental durability, repairability, manufacturing cost, and expected service life.
8. Manufacturing Considerations for PP Honeycomb Marine Panels
The manufacturing process has a direct effect on panel consistency and long-term performance.
Step 1: Material Inspection
Check the core’s dimensions, density, cell geometry, and surface condition.
The face sheets should also be inspected for thickness, flatness, cleanliness, and defects.
Step 2: Surface Preparation
Polypropylene has relatively low surface energy. Depending on the selected adhesive, surface treatment may be necessary to achieve reliable bonding.
Manufacturers should qualify the surface preparation process using the actual core grade and face-sheet material.
Step 3: Adhesive Application
The adhesive must be compatible with polypropylene and the selected face sheets.
Its application method, thickness, curing conditions, and environmental resistance should be controlled.
Step 4: Panel Assembly
The core and face sheets are assembled according to the design.
Edge reinforcements, inserts, and other local structural elements should be installed in the specified positions.
Step 5: Pressing and Curing
Pressure, temperature, and curing time must follow the requirements of the selected manufacturing system.
Excessive pressure may deform the core, while inadequate pressure or poor surface preparation may cause bonding defects.
Step 6: Finishing
The panel is trimmed to the required dimensions.
Exposed edges, penetrations, and cutouts are sealed or reinforced according to the application.
Step 7: Quality Control
Inspection may include dimensional checks, visual inspection, bond-integrity assessment, and mechanical testing.
For critical components, representative finished panels should be tested under appropriate conditions.
9. Quality Control and Relevant Testing Standards
Material data should be evaluated using documented test methods.
The following standards are examples of methods that may be relevant to composite sandwich panel development. The applicable edition, specimen configuration, and laboratory procedure should be confirmed before testing.
| Test Standard | Test Area | Potential Application |
|---|---|---|
| ASTM C365/C365M | Flatwise compressive properties of sandwich cores | Evaluating core compression behavior |
| ASTM C273/C273M | Core shear properties | Evaluating shear strength and shear modulus |
| ASTM C393/C393M | Flexural properties of sandwich constructions | Evaluating sandwich beam behavior |
| ASTM D7249/D7249M | Facesheet properties of sandwich constructions | Evaluating face-sheet behavior under long-beam flexure |
| ASTM D7766/D7766M | Damage resistance of sandwich constructions | Evaluating damage resistance using specified procedures |
The suitability of each method depends on the actual material system and the purpose of the test.
In addition to core and panel testing, marine projects may require environmental conditioning, fatigue assessment, fire testing, smoke testing, or other qualification procedures.
A supplier should not claim that a product complies with a particular standard unless the relevant evidence is available.
10. How to Select a PP Honeycomb Panel Supplier
Selecting a reliable supplier involves more than confirming dimensions and unit prices.
Marine manufacturers should evaluate the supplier’s technical capabilities, customization options, manufacturing consistency, and ability to support the intended application.
10.1 Confirm Product Specifications
Request a technical data sheet covering core density, cell size, core thickness, face-sheet material, finished panel thickness, and dimensional tolerances.
10.2 Request Mechanical Test Data
Where available, request core shear strength, compression strength, finished-panel flexural properties, and bonding test results.
Confirm the test methods and whether the data applies to the core or the complete panel.
10.3 Check Customization Capabilities
Determine whether the supplier can manufacture the required dimensions, face-sheet combinations, surface finishes, and reinforced attachment areas.
10.4 Evaluate Manufacturing Quality
Ask about incoming inspection, process controls, dimensional inspection, bonding quality checks, and product traceability.
10.5 Validate the Application
For critical marine applications, test prototypes under representative environmental and mechanical conditions before approving production.
This is particularly important for panels used in flooring, decks, load-bearing structures, or regulated interior systems.
11. Frequently Asked Questions
Q1. Are PP honeycomb panels suitable for boat interiors?
They can be suitable for selected boat interior applications, including wall panels, cabinet doors, partitions, and lightweight covers, provided that the panel meets the relevant mechanical, environmental, and regulatory requirements.
Q2. Are PP honeycomb panels waterproof?
Polypropylene itself has low water absorption, but the finished panel is not automatically waterproof. Face sheets, bonded interfaces, edges, fastener holes, and cutouts must be designed to prevent water ingress where required.
Q3. Can PP honeycomb panels replace plywood in yacht furniture?
They can replace plywood in some applications, particularly where reducing weight is important. However, the complete panel must provide adequate stiffness, fastening strength, surface durability, and local load resistance.
Q4. Can FRP be used as the face sheet?
Yes, FRP is one possible face-sheet material. The bonding system must be compatible with both the polypropylene core and the FRP surface, and the complete panel should be tested as required.
Q5. What panel thickness should marine manufacturers choose?
There is no universal thickness. Selection depends on panel span, support spacing, loading, face-sheet properties, core shear performance, deflection limits, and available installation space.
Q6. Are PP honeycomb panels suitable for boat decks?
They may be suitable for selected deck applications, but the design must verify bending, shear, local compression, impact resistance, water ingress protection, surface slip resistance, and fatigue performance.
Q7. What information should buyers provide when requesting a quotation?
Buyers should specify the intended application, panel dimensions, total thickness, core density, cell size, face-sheet material, surface finish, mechanical requirements, environmental conditions, and any applicable marine regulations.
12. Conclusion
PP honeycomb panels provide a potential lightweight composite solution for boat and yacht construction.
Their combination of polypropylene honeycomb core and suitable face sheets can reduce component weight while providing useful stiffness and design flexibility.
Potential applications include yacht furniture, cabin partitions, interior wall panels, access doors, equipment covers, and selected flooring structures.
Successful implementation depends on appropriate core selection, compatible bonding, adequate edge protection, proper structural design, and manufacturing quality control.
For marine manufacturers, the most effective approach is to define the component’s functional requirements first, compare complete panel constructions using verified data, and validate the selected design under representative service conditions.
Looking for Customized PP Honeycomb Panels for Boat and Yacht Manufacturing?
ONEBOND can evaluate project-specific requirements for PP honeycomb core and composite panel applications. When requesting a quotation, provide the required panel dimensions, total thickness, core density, face-sheet material, intended application, and mechanical performance requirements.
These details help establish the most appropriate product configuration for your marine composite manufacturing project.
