1. Introduction: The Growing Demand for Lightweight Marine Interior Panels
In modern boatbuilding and yacht manufacturing, reducing structural weight while maintaining sufficient strength, durability, and dimensional stability is an important engineering objective.
Traditional marine interior materials, such as plywood, solid wood boards, and conventional composite boards, have been widely used in boat interior walls, partitions, furniture, and flooring. However, these materials may present limitations related to weight, moisture exposure, dimensional stability, and long-term maintenance.
As marine composite technology continues to develop, PP honeycomb panels are becoming an alternative solution for selected lightweight interior applications.
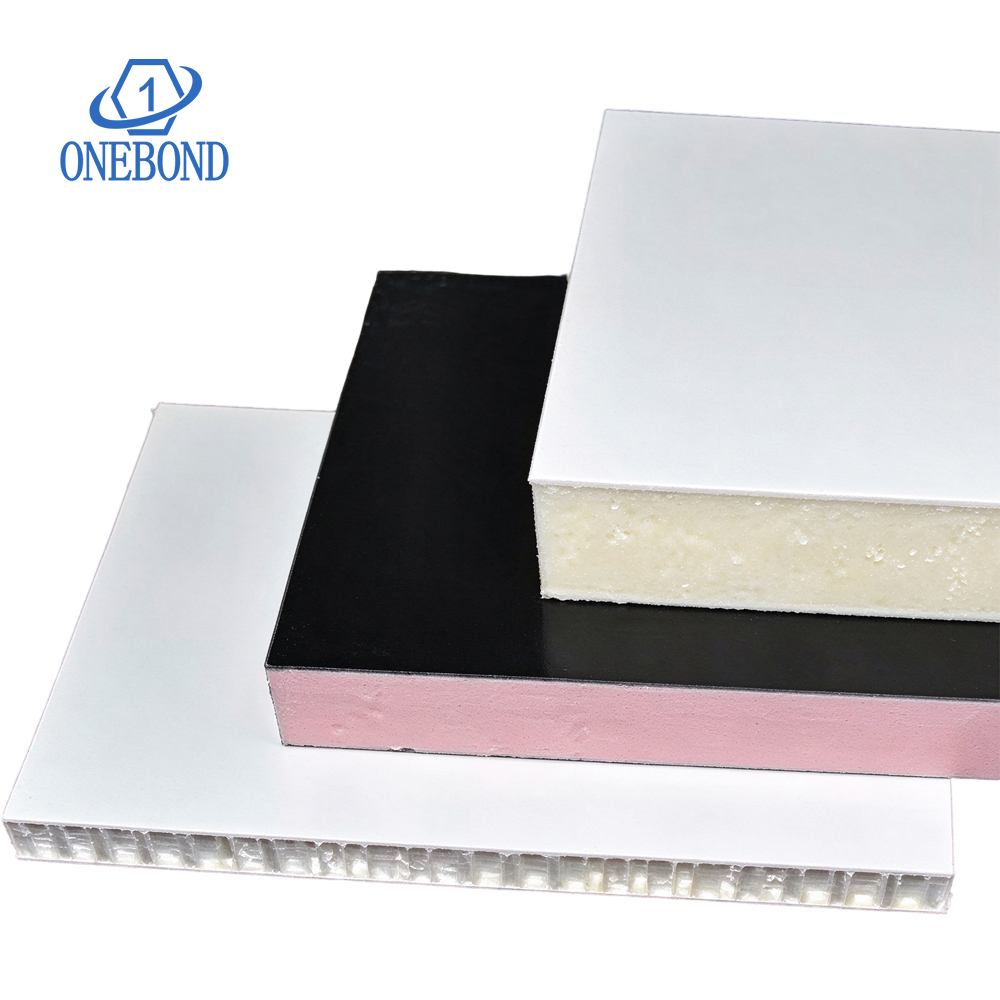
A PP honeycomb panel typically consists of a polypropylene honeycomb core bonded between two facing materials. Depending on the intended application, the skins can be fiberglass reinforced plastic (FRP), aluminum sheet, plywood, or other composite materials.
The resulting sandwich panel structure combines a lightweight cellular core with relatively rigid outer skins.
For marine applications, this structure can provide several advantages:
- Reduced panel weight compared with many traditional solid-board constructions.
- High bending stiffness relative to the weight of the panel.
- Good resistance to water absorption by the polypropylene core.
- Flexible panel thickness and skin configurations.
- Compatibility with different surface finishes and composite manufacturing processes.
- Potential for prefabricated wall, partition, furniture, and flooring components.
This article explains how PP honeycomb panels are used in boat interior walls, marine partitions, and flooring systems. It also discusses panel structures, material properties, manufacturing considerations, technical parameters, and purchasing criteria for marine composite panel manufacturers.
2. What Is a PP Honeycomb Panel?
A PP honeycomb panel is a lightweight sandwich composite panel that uses a polypropylene honeycomb core as its internal structural material.
The core consists of numerous interconnected cellular structures, usually with hexagonal or similar geometric configurations.
The honeycomb structure creates separation between the two outer skins. This separation increases the panel’s bending stiffness without requiring a solid material throughout its thickness.
2.1 Basic Structure of a Marine PP Honeycomb Sandwich Panel
A typical FRP-faced PP honeycomb panel contains three main components:
1. Top Skin
The upper facing layer provides surface protection, appearance, and part of the panel’s bending resistance. In marine applications, common options include fiberglass reinforced plastic, gelcoat FRP, and other composite laminates.
2. PP Honeycomb Core
The polypropylene honeycomb core provides lightweight structural support and maintains the distance between the two skins. Its thickness, density, cell size, and mechanical properties influence the performance of the finished panel.
3. Bottom Skin
The bottom facing layer provides additional stiffness and helps balance the sandwich structure. It may use the same material as the top skin or a different material depending on the application.
The bonding interface between the core and skins is also critical. A sandwich panel can only perform as intended when the adhesive system, surface preparation, and manufacturing process provide sufficient interfacial adhesion.
2.2 Common Marine PP Honeycomb Panel Configurations
| Panel Configuration | Main Materials | Typical Applications |
|---|---|---|
| FRP + PP Honeycomb + FRP | Fiberglass skins and PP core | Boat walls, partitions, flooring |
| Gelcoat FRP + PP Honeycomb + FRP | Gelcoat surface and PP core | Yacht interior panels |
| Aluminum + PP Honeycomb + Aluminum | Aluminum skins and PP core | Selected interior panels |
| Plywood + PP Honeycomb + FRP | Plywood, PP core, FRP | Customized furniture panels |
| Decorative Laminate + PP Honeycomb + FRP | Decorative surface and composite structure | Cabin furniture and interior decoration |
The appropriate configuration depends on panel dimensions, mechanical loads, surface requirements, fire performance, manufacturing methods, and the marine environment.
3. PP Honeycomb Panels for Boat Interior Walls
Boat interior walls are important components of marine accommodation spaces. They divide the interior into functional areas while contributing to the overall appearance, comfort, and usability of the vessel.
Common applications include:
- Cabin wall panels
- Interior lining panels
- Corridor wall panels
- Decorative wall boards
- Bathroom and washroom partitions
- Equipment compartment lining
- Yacht interior wall systems
3.1 Lightweight Boat Interior Wall Panels
Weight reduction is particularly important in boat and yacht construction because excessive interior weight can affect payload capacity, stability, fuel consumption, and vessel performance.
Traditional solid wood and plywood panels may be relatively heavy, especially when used across large interior surfaces.
A PP honeycomb sandwich panel can reduce the amount of solid material required while maintaining a rigid panel structure.
For example, an FRP-faced PP honeycomb panel can use a lightweight polypropylene core between two fiberglass skins. The skins provide the outer structural layers, while the honeycomb core supports the spacing between them.
The actual weight advantage depends on:
- PP honeycomb core density
- Core thickness
- FRP skin thickness
- Fiberglass reinforcement type
- Resin content
- Adhesive weight
- Additional reinforcement and finishing materials
For boat interior wall panels, manufacturers should evaluate the complete finished-panel weight rather than comparing core density alone.
3.2 Moisture Resistance for Marine Interior Walls
Marine interior environments can experience humidity, condensation, cleaning water, and occasional water exposure.
Polypropylene is a hydrophobic thermoplastic material with low water absorption. Therefore, PP honeycomb core can be suitable for composite structures where moisture resistance is an important consideration.
However, the moisture performance of the finished panel depends on more than the core material.
Important factors include:
- Skin material and surface finish
- Edge sealing quality
- Adhesive water resistance
- Panel joints and connections
- Cutout and fastener protection
- Long-term exposure conditions
For example, an FRP-faced PP honeycomb panel may offer good moisture resistance when its skins, bonding system, and edges are properly designed.
The core itself does not make the entire panel waterproof. Water can still enter through damaged skins, poorly sealed edges, joints, or penetrations.
3.3 Decorative Options for Yacht Interior Wall Panels
Marine interior design often requires both functional performance and an attractive appearance.
PP honeycomb panels can be manufactured with different facing materials and decorative finishes.
Common options include:
- White FRP surface
- Gelcoat fiberglass surface
- Wood-grain decorative laminate
- High-pressure laminate (HPL)
- PVC decorative film
- Aluminum sheet
- Customized composite facing materials
For yacht interior wall panels, manufacturers can select different colors, textures, surface gloss levels, and panel dimensions.
The choice of facing material should consider cleaning requirements, scratch resistance, chemical exposure, fire regulations, and the intended interior design.
4. PP Honeycomb Panels for Marine Partitions and Bulkhead Applications
Partitions divide the interior of boats and yachts into separate functional spaces. They can be used in cabins, bathrooms, storage areas, corridors, and equipment compartments.
The terms interior partition and structural bulkhead should not be treated as interchangeable.
A lightweight PP honeycomb partition panel may be suitable for non-primary interior divisions. A structural or watertight bulkhead, however, must meet the vessel’s specific structural, fire, and classification requirements.
4.1 Lightweight Marine Partition Panels
A PP honeycomb sandwich panel can provide a favorable stiffness-to-weight relationship compared with many solid-board alternatives.
The panel’s performance depends on the combined behavior of its skins, core, adhesive interface, and edge reinforcement.
For marine partition applications, engineers should consider:
- Panel height and width
- Unsupported span
- Panel thickness
- Core density and mechanical properties
- Skin material and thickness
- Connection details
- Impact and vibration exposure
- Openings for doors, windows, and equipment
Larger panels and panels with openings may require additional reinforcement to control deflection and prevent local damage.
4.2 FRP PP Honeycomb Panels for Cabin Partitions
FRP PP honeycomb panels are a practical material configuration for selected marine interior applications.
Fiberglass reinforced plastic skins provide a durable surface and can be manufactured in different thicknesses and finishes.
The PP honeycomb core provides lightweight internal support.
A typical manufacturing structure is:
FRP Skin + Adhesive Interface + PP Honeycomb Core + Adhesive Interface + FRP Skin
Depending on the production process, bonding can be achieved through adhesive bonding, vacuum-assisted processes, or other validated composite manufacturing methods.
For a reliable marine partition panel, manufacturers should verify:
- Skin-to-core bonding strength.
- Core shear performance.
- Panel bending performance.
- Resistance to environmental exposure.
- Edge reinforcement and connection strength.
- Fire, smoke, and toxicity compliance where required.
4.3 Can PP Honeycomb Panels Be Used for Watertight Bulkheads?
This question requires careful engineering consideration.
A PP honeycomb panel should not automatically be considered suitable for a watertight bulkhead simply because polypropylene has low water absorption.
A watertight bulkhead is a complete engineered assembly. Its performance depends on the panel structure, perimeter connections, penetrations, joints, doors, seals, and applicable marine regulations.
For a watertight application, the complete assembly must be designed and tested against the relevant requirements.
Unless the panel and installation system have been specifically engineered and approved for that purpose, PP honeycomb panels should be considered for non-primary interior partition applications rather than assumed to be suitable for watertight or primary structural bulkheads.
5. PP Honeycomb Panels for Boat Flooring Systems
Boat flooring is another potential application for lightweight PP honeycomb sandwich panels.
Floor panels must withstand distributed loads, concentrated loads, repeated foot traffic, vibration, and occasional impact.
Depending on the vessel design, they may also need to resist water exposure, cleaning chemicals, and temperature variations.
Common marine flooring applications include:
- Cabin flooring panels
- Yacht interior floorboards
- Raised access flooring
- Lightweight equipment platform panels
- Interior deck panels
- Removable floor sections
- Customized marine composite floorboards
5.1 Why Use PP Honeycomb Core for Boat Flooring?
The honeycomb core provides internal support while reducing the quantity of solid material used in the panel.
When properly engineered, an FRP-faced PP honeycomb sandwich panel can offer:
- Reduced weight compared with selected solid-panel constructions.
- A relatively high bending stiffness-to-weight ratio.
- Good moisture resistance of the polypropylene core.
- Flexible panel thickness and skin design.
- Compatibility with different anti-slip and decorative surfaces.
However, flooring performance is highly dependent on panel design.
A floor panel with insufficient core shear strength, inadequate skin thickness, or poorly designed supports may experience excessive deflection, local crushing, skin damage, or delamination.
5.2 Anti-Slip Surface Options for Marine Flooring
Slip resistance is an important consideration for marine flooring, especially in areas exposed to water.
Common surface options include:
| Surface Material | Main Characteristics | Potential Applications |
|---|---|---|
| Anti-slip FRP | Textured surface, composite construction | Boat interior flooring |
| Molded FRP | Integrated surface texture | Marine floor panels |
| Non-slip gelcoat | Decorative finish with selected texture | Yacht interior floors |
| Rubber flooring | Flexible surface and foot comfort | Cabin flooring |
| PVC flooring | Decorative and easy-to-clean surface | Interior floor coverings |
| Aluminum tread plate | Textured metal surface | Selected equipment and access areas |
The surface layer should be selected according to slip resistance, abrasion resistance, cleaning requirements, bonding compatibility, and applicable fire regulations.
A PP honeycomb core does not itself provide an anti-slip surface. The surface material and its attachment to the sandwich panel determine the finished flooring surface characteristics.
5.3 Load-Bearing Considerations for Boat Flooring Panels
For flooring applications, selecting a PP honeycomb core based only on density is insufficient.
The core must be evaluated for compression and shear behavior, while the complete panel must be evaluated for bending and deflection.
Important design variables include:
- Core thickness
- Core density
- Cell size and cell geometry
- Core compression strength
- Core shear strength
- FRP skin thickness
- Skin tensile and flexural properties
- Support spacing
- Concentrated load distribution
- Edge and insert reinforcement
A higher-density core may provide greater mechanical strength in some grades, but this relationship is not universal. Core structure, polymer formulation, manufacturing quality, and test direction also influence performance.
For flooring systems, the complete sandwich panel should be tested under representative support and loading conditions.
6. Technical Parameters of PP Honeycomb Panels for Marine Applications
The technical performance of a marine PP honeycomb panel depends on both the core and the finished sandwich construction.
The following tables provide a practical specification framework for manufacturers and procurement teams. They are not certified product specifications or universal standard values.
6.1 PP Honeycomb Core Parameters
| Parameter | Typical Specification Description | Why It Matters |
|---|---|---|
| Material | Polypropylene (PP) | Defines the base polymer |
| Core Structure | Honeycomb cellular structure | Determines internal geometry |
| Core Density | Specified in kg/m³ | Affects weight and mechanical performance |
| Core Thickness | Customized according to design | Influences panel thickness and stiffness |
| Cell Size | Customized according to requirements | Influences structural behavior and processing |
| Compression Strength | Tested value in MPa | Important for local compression and support |
| Shear Strength | Tested value in MPa | Important for sandwich-panel load transfer |
| Shear Modulus | Tested value in MPa | Influences panel deformation |
| Water Absorption | Tested according to an agreed method | Helps assess moisture behavior |
| Surface Treatment | Untreated or bonding-treated | Important for adhesive compatibility |
| Color | Natural or customized | Identification and production requirements |
6.2 Finished Marine Sandwich Panel Parameters
| Parameter | Specification Options | Application Considerations |
|---|---|---|
| Panel Structure | FRP + PP Honeycomb + FRP | Common lightweight composite configuration |
| Panel Thickness | Customized | Depends on span and loading |
| Core Thickness | Customized | Influences weight and stiffness |
| FRP Skin Thickness | Customized | Influences bending and impact performance |
| Surface Finish | Gelcoat, smooth FRP, textured FRP | Depends on interior design and use |
| Panel Width | Customized | Depends on vessel layout |
| Panel Length | Customized | Depends on manufacturing and installation |
| Panel Weight | kg/m², measured on finished panel | Important for vessel weight control |
| Flexural Strength | Tested value | Evaluates bending behavior |
| Core Shear Strength | Tested value | Evaluates internal load transfer |
| Bonding Strength | Tested value | Evaluates skin-to-core adhesion |
| Fire Performance | Project-specific requirement | Must comply with applicable regulations |
6.3 Example Technical Specification for a Customized Boat Interior Panel
The following is an example of how a procurement specification can be organized. Actual dimensions and performance values must be confirmed by engineering calculations and testing.
| Item | Example Requirement |
|---|---|
| Product Name | FRP PP Honeycomb Marine Sandwich Panel |
| Application | Boat Interior Wall and Partition |
| Face Material | Fiberglass Reinforced Plastic |
| Core Material | Polypropylene Honeycomb |
| Core Thickness | 15–30 mm, illustrative design range |
| FRP Skin Thickness | To be determined by structural design |
| Surface Finish | Smooth or gelcoat |
| Panel Dimensions | Customized |
| Core Surface | Bonding treatment as required |
| Edge Treatment | Sealed or reinforced according to design |
| Fire Requirements | According to vessel and project specifications |
| Testing | Agreed mechanical and environmental tests |
For boat flooring, the specification should additionally define the design load, support spacing, maximum allowable deflection, anti-slip requirements, and concentrated-load test conditions.
7. PP Honeycomb Core vs Plywood and PVC Foam Core for Marine Interior Panels
Different core and panel materials have different performance characteristics. The most appropriate choice depends on the application rather than a single material property.
| Comparison Factor | PP Honeycomb Core | PVC Foam Core | Plywood |
|---|---|---|---|
| Material Structure | Cellular honeycomb | Closed-cell polymer foam | Layered wood veneer |
| Core Weight | Depends on density and thickness | Depends on density and thickness | Depends on wood species and construction |
| Water Absorption | Generally low for PP material | Generally low for closed-cell grades | Depends strongly on grade and sealing |
| Stiffness | Depends on sandwich design and skins | Depends on density, thickness, and skins | Depends on veneer structure and thickness |
| Core Shear Behavior | Grade- and geometry-dependent | Grade-dependent | Depends on wood structure |
| Bonding Requirements | Surface treatment may be necessary | Depends on foam chemistry and adhesive | Depends on surface and adhesive |
| Machining | Requires suitable cutting and edge treatment | Generally machinable | Generally easy to machine |
| Typical Applications | Lightweight partitions, interior panels, selected flooring | Marine sandwich structures and composite panels | Furniture, interior construction, selected structural uses |
7.1 PP Honeycomb Core vs PVC Foam Core
PP honeycomb core and PVC foam core are both used in lightweight composite panel manufacturing, but their cellular structures are different.
PP honeycomb core uses a geometric honeycomb structure. Its mechanical performance depends on cell geometry, material grade, density, and loading direction.
PVC foam core uses a cellular foam structure. Its mechanical properties depend on foam density, cell structure, formulation, and manufacturing quality.
For boat interior walls and partitions, both materials may be suitable depending on the panel design.
For flooring and applications with significant mechanical loads, manufacturers should compare compression strength, shear strength, flexural behavior, and finished-panel performance.
Neither material should be selected based on density alone.
7.2 PP Honeycomb Core vs Plywood
Plywood is widely used in traditional boat interiors because it is relatively easy to cut, shape, fasten, and finish.
However, wood-based panels may require appropriate sealing and protection against moisture exposure.
PP honeycomb sandwich panels provide a different construction approach. They can reduce the amount of solid material used and offer a lightweight composite structure.
The main consideration is that sandwich panels require suitable bonding, edge detailing, and connection design. They may not accept conventional screws and fasteners in the same way as solid plywood.
For marine furniture and interior installations, local reinforcement or dedicated inserts may be required.
8. Manufacturing Process of FRP PP Honeycomb Marine Panels
The manufacturing process has a major influence on the final quality and performance of PP honeycomb sandwich panels.
A typical production workflow includes the following stages.
Step 1: PP Honeycomb Core Preparation
The manufacturer selects the appropriate polypropylene honeycomb core according to the required thickness, density, cell size, and mechanical properties.
The core should be inspected for:
- Thickness consistency
- Surface flatness
- Cell structure uniformity
- Visible damage
- Contamination
- Dimensional accuracy
Step 2: Core Surface Treatment
Polypropylene has relatively low surface energy, which can make direct adhesive bonding difficult.
Depending on the adhesive system and manufacturing process, surface treatment may be required.
Common approaches include:
- Corona treatment
- Plasma treatment
- Flame treatment
- Compatible primer systems
- Other validated surface preparation methods
The appropriate treatment should be confirmed through adhesive compatibility testing and production trials.
Step 3: FRP Skin Preparation
Fiberglass skins are prepared according to the panel design.
The manufacturer selects suitable laminate thickness, resin system, reinforcement type, and surface finish.
For marine interior applications, the skin should meet the required appearance, mechanical performance, and environmental durability.
Step 4: Adhesive Application
A suitable adhesive system is applied to the bonding surfaces.
The adhesive should be compatible with both the PP honeycomb core and the facing material.
Important manufacturing controls include:
- Adhesive application quantity
- Mixing ratio where applicable
- Open time
- Working temperature
- Bond-line uniformity
- Curing conditions
Step 5: Sandwich Panel Assembly
The upper skin, PP honeycomb core, and lower skin are assembled into the designed sandwich structure.
Care should be taken to maintain alignment, avoid core displacement, and achieve uniform adhesive coverage.
Step 6: Pressing and Curing
The assembled panel is pressed using an appropriate process.
Vacuum pressing, flat-bed pressing, or other suitable production methods may be selected according to panel construction and adhesive requirements.
Pressure, temperature, and curing time must follow the validated manufacturing procedure.
Excessive pressure may damage the core, while insufficient pressure may result in incomplete bonding.
Step 7: Cutting and Edge Finishing
After curing, the panel is cut to the required dimensions.
Edges may require sealing, reinforcement, or additional inserts depending on the installation design.
Cutouts for doors, windows, cable routes, and equipment should be considered during engineering design.
Step 8: Quality Inspection
Finished panels should be inspected for:
- Overall thickness
- Length and width
- Flatness
- Surface defects
- Weight per square meter
- Skin-to-core bonding
- Mechanical performance
- Edge quality
For marine applications, the inspection plan should also include project-specific environmental and fire-performance requirements.
9. Key Quality Tests for Marine PP Honeycomb Sandwich Panels
A reliable marine sandwich panel should be evaluated as a complete composite structure.
Testing only the PP honeycomb core does not fully establish the performance of the finished panel.
Depending on the application, the following standards and test methods may be relevant.
| Test Standard | Test Subject | Potential Relevance |
|---|---|---|
| ASTM C365/C365M | Flatwise compressive properties of sandwich cores | Core compression behavior |
| ASTM C273/C273M | Shear properties of sandwich core materials | Core shear behavior |
| ASTM C393/C393M | Core shear properties of sandwich constructions by beam flexure | Sandwich construction behavior |
| ASTM D7249/D7249M | Facing properties of sandwich constructions by long-beam flexure | Facing response under bending |
| ASTM D7766/D7766M | Damage resistance of sandwich constructions | Impact and damage evaluation |
The current edition, specimen configuration, material applicability, and laboratory procedure should be confirmed before specifying any test.
For an actual boat or yacht project, the buyer should also identify the applicable marine classification rules, statutory requirements, and vessel-specific fire and structural requirements.
9.1 Bonding Strength Testing
Bonding quality is particularly important for FRP PP honeycomb panels.
Poor adhesion can cause skin-to-core delamination, which may reduce bending stiffness and compromise the panel’s service life.
Bonding evaluation should consider:
- Adhesive compatibility
- Surface treatment effectiveness
- Peel or cleavage behavior where relevant
- Failure mode
- Bonding consistency across the panel
A suitable test method should be agreed between the manufacturer and buyer.
9.2 Compression and Shear Testing
Boat flooring and partition panels may experience different loading conditions.
Compression testing helps evaluate the core’s resistance to through-thickness loading.
Shear testing helps evaluate the core’s ability to transfer loads between the skins.
Both properties are important when selecting a PP honeycomb core for sandwich panel manufacturing.
9.3 Environmental and Fire Performance
Marine panels may be exposed to humidity, temperature changes, cleaning chemicals, vibration, and occasional water contact.
Environmental testing should reflect the expected service conditions.
Fire performance is a separate and particularly important consideration.
Polypropylene is a thermoplastic polymer and should not automatically be considered fire-resistant. A fire-retardant grade or a specially designed panel structure does not automatically establish compliance with marine fire regulations.
Where required, the complete panel assembly must be evaluated against the applicable fire, smoke, and toxicity requirements.
10. How to Select the Right PP Honeycomb Core for Boat Interior Panels
Selecting the right PP honeycomb core requires matching the material’s properties to the finished panel’s intended function.
10.1 Select Core Density According to Mechanical Requirements
Core density influences material weight and often correlates with mechanical performance, but it is not a complete indicator of quality.
Buyers should request actual compression and shear test data for the selected grade.
For lightweight interior walls, the design requirements may differ significantly from those of flooring panels.
10.2 Select Core Thickness According to Panel Span
Core thickness is an important design variable.
Increasing core thickness can improve sandwich-panel bending stiffness when the skins and bonding system are appropriately designed.
However, a thicker core also increases panel thickness and may affect edge details, connections, and installation space.
The correct thickness should be determined according to:
- Unsupported panel span
- Design loading
- Allowable deflection
- Skin properties
- Support arrangement
- Installation requirements
10.3 Consider Cell Size and Geometry
Honeycomb cell size and geometry can influence core behavior, bonding contact, cutting, and processing.
The appropriate structure depends on the required mechanical performance and manufacturing method.
Buyers should specify cell geometry and dimensional tolerances rather than assuming that all PP honeycomb cores are equivalent.
10.4 Confirm Bonding Compatibility
One of the most important purchasing considerations is whether the selected PP honeycomb core can be reliably bonded to the intended FRP or other facing material.
The buyer should confirm:
- Whether the core has received surface treatment
- Which adhesive systems have been validated
- Whether production trials have been completed
- Whether finished-panel bonding tests are available
10.5 Confirm Marine Fire and Environmental Requirements
Before ordering a PP honeycomb core or finished marine panel, identify the relevant vessel type, installation location, and regulatory requirements.
For example, a decorative cabin partition and a panel installed in a regulated passenger-vessel space may have very different fire-performance requirements.
A supplier should not claim universal marine certification based solely on the material name or a generic test report.
11. Common Problems When Purchasing PP Honeycomb Panels for Marine Applications
Marine composite panel buyers should pay attention to several issues before placing a bulk order.
Problem 1: Choosing a Core Based Only on Density
Two PP honeycomb cores with the same nominal density may have different mechanical properties because of differences in cell geometry, polymer formulation, and production quality.
Recommendation: Request compression and shear test reports for the specific grade.
Problem 2: Ignoring the Bonding Interface
PP has low surface energy, so bonding performance requires careful consideration.
Recommendation: Confirm surface treatment and adhesive compatibility before mass production.
Problem 3: Comparing Core Weight Instead of Finished Panel Weight
A lightweight core does not necessarily produce the lightest finished panel.
Thicker FRP skins, heavy adhesives, edge reinforcement, and decorative finishes all contribute to the final weight.
Recommendation: Compare finished-panel weight in kg/m² using equivalent panel dimensions and performance requirements.
Problem 4: Overlooking Edge Sealing
Even if the PP core itself has low water absorption, water can enter through exposed edges and damaged facing materials.
Recommendation: Define edge sealing and penetration protection in the panel specification.
Problem 5: Ignoring Fire Compliance
A lightweight PP honeycomb panel is not automatically suitable for every marine interior location.
Recommendation: Confirm the required fire, smoke, and toxicity performance of the complete panel assembly.
Problem 6: Using Interior Panels for Structural Applications Without Verification
A panel suitable for a decorative partition may not be suitable for a structural bulkhead or load-bearing floor.
Recommendation: Define the design loads and obtain engineering verification before using the panel in a structural application.
12. What Should Marine Panel Manufacturers Ask Their PP Honeycomb Core Supplier?
For composite panel manufacturers, selecting a stable PP honeycomb core supplier is important for production consistency and finished-panel quality.
The following checklist can help procurement teams evaluate suppliers.
| Purchasing Question | Why It Matters |
|---|---|
| What PP honeycomb core densities are available? | Helps identify suitable material grades |
| What core thicknesses can be supplied? | Supports different panel designs |
| What cell sizes are available? | Helps match mechanical and processing requirements |
| Can the core be supplied with surface treatment? | Supports bonding compatibility |
| Are compression and shear test reports available? | Provides technical verification |
| Can customized dimensions be produced? | Improves production efficiency |
| Is sample production available? | Allows manufacturing trials |
| Can technical support be provided? | Helps solve material and process issues |
| Can batch consistency be controlled? | Reduces finished-panel variation |
| Can the supplier support long-term orders? | Supports stable production planning |
For buyers producing FRP PP honeycomb marine panels, a supplier should be able to provide clear technical specifications, material samples, production support, and consistent quality documentation.
13. Frequently Asked Questions About PP Honeycomb Panels for Boats
Q1: What Is a PP Honeycomb Panel Used for in Boat Building?
PP honeycomb panels are used in selected lightweight marine interior applications, including cabin wall panels, non-primary partitions, furniture panels, interior flooring, and other composite components.
Their suitability depends on the core grade, facing materials, panel thickness, bonding system, mechanical loading, and marine regulatory requirements.
Q2: Are PP Honeycomb Panels Waterproof?
Polypropylene has low water absorption, making PP honeycomb core suitable for applications where moisture resistance is important.
However, the finished panel is not automatically waterproof. Its moisture performance depends on the facing materials, adhesive, edge sealing, joints, and installation details.
Q3: Can PP Honeycomb Core Be Bonded with FRP Sheets?
Yes, PP honeycomb core can be incorporated into FRP-faced sandwich panels.
Because polypropylene has relatively low surface energy, the bonding system may require surface treatment, a compatible adhesive, or a validated primer system.
Bonding performance should be verified through production trials and appropriate testing.
Q4: Is PP Honeycomb Panel Suitable for Boat Flooring?
PP honeycomb panels can be designed for selected boat flooring applications.
The finished panel must be engineered for the expected distributed and concentrated loads, support spacing, deflection limits, core shear behavior, skin strength, and surface requirements.
Q5: What Is the Difference Between PP Honeycomb Core and PVC Foam Core?
PP honeycomb core has a geometric cellular structure, while PVC foam core has a foam-cell structure.
Their mechanical behavior, bonding requirements, weight, and manufacturing characteristics differ.
The best choice depends on the application and the performance of the complete sandwich panel.
Q6: Can PP Honeycomb Panels Be Customized for Yacht Interiors?
Yes. PP honeycomb sandwich panels can be customized in core thickness, density, cell size, facing material, surface finish, and panel dimensions.
For yacht interiors, customization may include decorative FRP skins, gelcoat finishes, wood-grain laminates, and other facing materials.
Q7: Are PP Honeycomb Panels Fireproof?
No. Standard polypropylene is combustible and should not be described as fireproof.
Fire-retardant formulations and specially designed composite structures may improve fire performance, but compliance must be verified through applicable testing of the complete panel assembly.
Q8: How Can I Choose the Right PP Honeycomb Core for Marine Composite Panels?
Start by identifying the application, design load, panel dimensions, thickness, skin material, and environmental requirements.
Then compare core density, compression strength, shear strength, cell size, surface treatment, and finished-panel test results.
The selection should be based on verified performance rather than density or price alone.
14. Why Choose a Professional PP Honeycomb Core Manufacturer?
For marine composite panel manufacturers, the quality of the core material directly affects production stability and finished-panel performance.
A professional PP honeycomb core manufacturer should provide:
- Consistent core density and thickness.
- Stable honeycomb cell geometry.
- Customized dimensions and specifications.
- Technical data and mechanical test information.
- Bonding surface treatment options.
- Reliable production capacity.
- Technical support for composite panel manufacturing.
- Stable supply for long-term cooperation.
For companies manufacturing boat interior wall panels, marine partitions, and lightweight flooring panels, working with an experienced PP honeycomb core supplier can help improve material selection and production efficiency.
ONEBOND focuses on composite core materials and lightweight sandwich panel solutions, including PP honeycomb core and other foam core materials. For marine composite applications, buyers can evaluate customized PP honeycomb core specifications according to their panel structure, production process, and application requirements.
15. Conclusion: PP Honeycomb Panels as a Lightweight Solution for Marine Interior Construction
PP honeycomb panels provide a lightweight sandwich structure for selected boat and yacht interior applications.
When combined with suitable facing materials such as FRP, they can be used to manufacture cabin wall panels, non-primary partitions, furniture components, and engineered flooring panels.
Their key advantages include low core water absorption, lightweight construction, flexible panel configurations, and compatibility with different composite manufacturing processes.
However, successful marine applications require more than selecting a polypropylene honeycomb core.
Core density, cell geometry, panel thickness, skin materials, adhesive compatibility, edge sealing, mechanical loading, and fire-performance requirements must all be considered.
For marine panel manufacturers and procurement professionals, the most effective approach is to select PP honeycomb core according to the finished panel’s actual engineering requirements and verify performance through appropriate testing.
With suitable material selection and manufacturing control, PP honeycomb sandwich panels can become a valuable option for lightweight marine interior construction.
SEO Publishing Recommendations
Recommended URL Slug:
/pp-honeycomb-panels-boat-interior-walls-partitions-flooring/
Primary Keyword: PP Honeycomb Panels for Boat Interior Walls
Recommended H1:
PP Honeycomb Panels for Boat Interior Walls, Partitions, and Flooring
Suggested Image Alt Text:
- PP Honeycomb Panel for Boat Interior Wall
- FRP PP Honeycomb Sandwich Panel for Marine Applications
- Lightweight PP Honeycomb Marine Partition Panel
- PP Honeycomb Core for Boat Flooring Panel
- Fiberglass Faced PP Honeycomb Panel for Yacht Interior
- Marine PP Honeycomb Sandwich Panel Manufacturing Process
Recommended Internal Links:
| Anchor Text | Suggested Target Page |
|---|---|
| PP Honeycomb Core | PP Honeycomb Core Product Page |
| PVC Foam Core | PVC Foam Core Product Page |
| PET Foam Core | PET Foam Core Product Page |
| Marine Sandwich Panel | Marine Composite Panel Application Page |
| FRP Honeycomb Panel | FRP Honeycomb Panel Product Page |
| Composite Core Materials | Composite Core Materials Category Page |
Recommended Related Article Links:
- PP Honeycomb Core for Marine Applications: Properties, Benefits, and Material Selection
- How PP Honeycomb Panels Improve Lightweight Boat and Yacht Construction
- PP Honeycomb Core vs PVC Foam Core for Marine Sandwich Panels
- How to Select PP Honeycomb Core for Marine Composite Panel Manufacturing
SEO Content Strategy:
Use the primary keyword in the H1, opening paragraph, one or two relevant H2 headings, image alt text, and meta description. Use secondary keywords naturally in the sections where they match the subject.
Avoid placing every keyword in every paragraph. Google search relevance is better supported by clear topical coverage, useful technical explanations, meaningful internal links, and content that satisfies the searcher’s actual intent.
The article should link to the corresponding product pages using descriptive anchor text, especially the PP Honeycomb Core and FRP PP Honeycomb Panel pages. This helps search engines understand the relationship between the material, its applications, and the company’s product offerings.
