A Structural Optimization and Lightweight Design Report for Composite Sandwich Panels
1. Introduction: Thickness and Density Are Two Different Design Levers
When engineers select PVC Foam Core for a composite sandwich panel, two questions appear repeatedly:
Should we increase the core density?
or:
Should we increase the core thickness?
These two changes can both improve structural performance, but they do so through different mechanisms.
Increasing density primarily changes the intrinsic mechanical properties of the core, including:
- Compression strength
- Shear strength
- Shear modulus
- Compression modulus
- Local load capacity
Increasing thickness changes the geometry of the sandwich structure, especially the separation between the face sheets.
This distinction is fundamental.
A higher-density PVC Foam Core may provide greater local strength, while a thicker lower-density core may provide substantially greater sandwich bending stiffness with less weight penalty.
Therefore, the engineering optimization problem is not:
“Which PVC Foam Core density is strongest?”
It is:
“What combination of core density and thickness provides the required stiffness, strength, weight and manufacturing performance?”
ASTM C273/C273M is commonly used to characterize core shear strength and shear modulus, while ASTM C393/C393M evaluates the behavior of sandwich constructions under flexure. ASTM C365/C365M addresses flatwise compression properties of sandwich cores. (store.astm.org)
2. The Basic Sandwich Structure
A simplified sandwich panel consists of:
Face Sheet
↓
PVC Foam Core
↓
Face Sheet
The face sheets carry most of the tensile and compressive bending stresses.
The PVC Foam Core performs several important functions:
- Maintains face-sheet separation
- Transfers transverse shear
- Supports the face sheets
- Resists local compression
- Stabilizes the skins against buckling
- Contributes to overall panel stiffness
The structural efficiency comes largely from the distance between the face sheets.
This is why core thickness can have such a strong effect on bending stiffness.
3. Why Core Thickness Has a Large Effect on Bending Stiffness
For a simplified symmetric sandwich beam, bending stiffness is approximately related to:
[
D \approx 2E_f t_f \left(\frac{h}{2}\right)^2
]
where:
- (D) = bending stiffness
- (E_f) = face-sheet modulus
- (t_f) = face-sheet thickness
- (h) = distance between the face-sheet centroids
Because the distance between the face sheets is squared, increasing the sandwich depth can produce a large increase in bending stiffness.
This creates an important engineering principle:
Core thickness is primarily a geometric stiffness lever.
Density, in contrast, is primarily a material-property lever.
4. Thickness vs Density: The Fundamental Difference
| Design Change | Main Effect | Typical Benefit |
|---|---|---|
| Increase Density | Higher core properties | Strength and local load capacity |
| Increase Thickness | Greater skin separation | Bending stiffness |
| Increase Face Sheet | Higher skin capacity | Tensile/compressive strength |
| Increase Adhesive Quality | Better interface | Load transfer |
| Add Local Reinforcement | Local capacity | Inserts/load zones |
The correct solution depends on the governing failure mode.
5. Engineering Density Framework
The following density ranges can be used as a preliminary selection framework.
They are not universal specifications; actual mechanical values must be confirmed for the selected PVC Foam Core grade.
| Density | General Classification | Typical Structural Position |
|---|---|---|
| 45–60 kg/m³ | Ultra-light | Low-load panels |
| 60–80 kg/m³ | Lightweight structural | General sandwich structures |
| 80–100 kg/m³ | Medium structural | Higher-load panels |
| 100–130 kg/m³ | High structural | Local high-load areas |
| 130–160 kg/m³ | High-density | Concentrated loads |
| 160–200 kg/m³ | Very high-density | Severe local loading |
| >200 kg/m³ | Special-purpose | Inserts/local reinforcement |
The density alone does not define the suitability of a grade.
The engineer must compare density with:
- core thickness,
- core shear modulus,
- core shear strength,
- compression strength,
- panel dimensions,
- face-sheet properties,
- load case.
6. Engineering Thickness Framework
PVC Foam Core is available in many thicknesses, depending on the manufacturing and application requirements.
A preliminary design matrix can be organized as follows:
| Core Thickness | Typical Structural Role |
|---|---|
| 5 mm | Thin lightweight panels |
| 10 mm | Interior/low-load structures |
| 15 mm | Moderate sandwich construction |
| 20 mm | General structural panels |
| 25–30 mm | Higher stiffness |
| 40–50 mm | High stiffness sandwich |
| 60–80 mm | Deep structural sandwich |
| >80 mm | Specialized structures |
Thickness should never be selected independently from density.
7. A Simple Engineering Comparison
Consider two conceptual designs.
Design A
80 kg/m³ PVC Foam Core × 30 mm
Design B
120 kg/m³ PVC Foam Core × 20 mm
Design B has significantly higher core density.
But Design A has a thicker structural depth.
Depending on the face-sheet laminate and loading condition, Design A may provide better bending stiffness despite having a lower-density core.
This illustrates why:
Higher density does not automatically mean higher panel stiffness.
8. Core Mass Calculation
Core mass can be estimated as:
[
M_c = \rho_c V_c
]
For a flat panel:
[
M_c = \rho_c A t_c
]
where:
- (M_c) = core mass
- (\rho_c) = core density
- (A) = panel area
- (t_c) = core thickness
Therefore, increasing thickness directly increases core mass.
Increasing density also directly increases mass.
The optimization problem is to determine which increase produces the most useful structural performance per unit of added mass.
9. Specific Structural Efficiency
One useful engineering concept is:
[
\eta = \frac{\text{Structural Performance}}{\text{Added Mass}}
]
For bending-dominated sandwich panels, increasing thickness can provide a particularly favorable stiffness-to-weight improvement because of the geometric leverage created by separating the face sheets.
For compression- or shear-dominated structures, increasing density may become more attractive.
Thus:
Bending Dominated
Thickness becomes increasingly important.
Shear Dominated
Core shear modulus and strength become increasingly important.
Point Load Dominated
Compression strength and local density become increasingly important.
10. Load Case Determines the Optimization Strategy
| Dominant Load | Primary Design Variable |
|---|---|
| Global Bending | Core Thickness |
| Core Shear | Density + Thickness |
| Point Load | Density + Local Reinforcement |
| Compression | Density + Face Sheet |
| Buckling | Thickness + Core Modulus |
| Fatigue | Complete Sandwich System |
| Impact | Core Structure + Facesheets |
| Fastener Load | Local High-Density Core |
| Long Span | Thickness + Shear Modulus |
This table is more useful than a simple density ranking.
11. Bending-Dominated Panel Design
For a panel carrying distributed transverse loads, bending stiffness often governs.
Increasing core thickness:
5 mm → 10 mm → 20 mm → 30 mm
can substantially increase the structural depth.
The face sheets move farther apart, which increases the panel’s second moment of area.
This is why a lightweight, thick-core sandwich panel can outperform a thin, dense-core panel in bending-dominated applications.
Typical examples include:
- Marine decks
- Vehicle floors
- Large wall panels
- Wind turbine shells
- Transportation roofs
- Industrial platforms
12. Shear-Dominated Panel Design
When the panel is short, heavily loaded or subjected to high transverse shear, core shear performance becomes more important.
The engineer should evaluate:
- Core shear strength
- Core shear modulus
- Core thickness
- Panel span
- Load distribution
ASTM C273/C273M provides a standardized method for determining core shear properties. (store.astm.org)
ASTM C393/C393M can then be used to evaluate the complete sandwich construction.
This distinction is important because a core may have excellent bare-core properties but behave differently after bonding into a real sandwich.
13. Core Shear Area and Thickness
A simplified relationship is:
[
\tau = \frac{V}{b t_c}
]
where:
- (V) = transverse shear force
- (b) = panel width
- (t_c) = core thickness
Increasing core thickness increases the effective shear area.
Therefore, thickness can improve both:
- bending stiffness,
- shear capacity,
although the exact response depends on the sandwich geometry and failure mechanism.
This is one reason why increasing thickness can sometimes be more efficient than simply increasing density.
14. Compression-Dominated Design
For concentrated loads, density becomes more important.
Suppose a panel carries a heavy machine support.
The load is transferred through a relatively small area.
The core experiences local compression.
In this situation:
Core Thickness Alone May Not Be Enough
The engineer may require:
- Higher-density PVC Foam Core
- Local insert
- Load-spreading plate
- Higher-density core patch
- Structural laminate reinforcement
This creates the concept of density zoning.
15. Density Zoning
Instead of using one density throughout the panel:
Low Density
→ large general area
Medium Density
→ structural load zones
High Density
→ inserts and concentrated loads
This can reduce overall panel mass while maintaining local strength.
| Zone | Example Density Strategy |
|---|---|
| General Panel | 60–80 kg/m³ |
| Structural Region | 80–120 kg/m³ |
| High Load | 120–160 kg/m³ |
| Insert | 160–250+ kg/m³ |
| Edge | Medium/high density |
Actual values must be validated against the structural design.
16. Thickness Zoning
Thickness can also be varied.
For example:
| Panel Zone | Example Core Thickness |
|---|---|
| Low-load edge | 10–20 mm |
| General area | 20–30 mm |
| High-stiffness zone | 30–50 mm |
| Structural transition | 40–60 mm |
| Local reinforcement | Custom |
Thickness zoning can provide additional weight optimization.
However, thickness transitions must be designed carefully because abrupt changes can generate stress concentrations.
17. Combined Density + Thickness Optimization
The most advanced design uses both variables.
For example:
Zone A
60 kg/m³ × 30 mm
Zone B
80 kg/m³ × 30 mm
Zone C
120 kg/m³ × 25 mm
Zone D
160 kg/m³ × 20 mm
The objective is not to make the whole panel identical.
The objective is to create a structurally optimized material map.
18. Parameter Comparison Matrix
A conceptual comparison:
| Configuration | Density | Thickness | Relative Mass | Stiffness Potential | Local Strength |
|---|---|---|---|---|---|
| A | 60 kg/m³ | 20 mm | Low | Medium | Low |
| B | 60 kg/m³ | 30 mm | Medium | High | Low–Medium |
| C | 80 kg/m³ | 20 mm | Medium | Medium | Medium |
| D | 80 kg/m³ | 30 mm | Medium–High | High | Medium |
| E | 120 kg/m³ | 20 mm | High | Medium | High |
| F | 120 kg/m³ | 30 mm | Very High | Very High | High |
The correct selection depends on which performance parameter governs.
19. Real Engineering Case — Wind Turbine Blade Sandwich Structures
Wind turbine blades provide an excellent example of thickness-density optimization.
Blade shells are subjected to:
- aerodynamic loads,
- bending,
- shear,
- compression,
- cyclic fatigue,
- local buckling.
Research on wind turbine blade sandwich structures has shown that foam density and core machining configuration influence structural response and failure mechanisms. (sciencedirect.com)
For such structures, simply specifying:
“Use the highest-density PVC Foam Core”
would not necessarily be the optimal solution.
A more rational approach is:
Low-density core → low-load aerodynamic regions
Medium-density core → general shell
Higher-density core → high-load structural regions
Local reinforcement → concentrated load areas
20. Real Engineering Case — Tapered Sandwich Transition
A tapered PVC Foam Core structure provides another example of thickness optimization.
Published experimental research investigated tapered PVC Foam Core sandwich specimens representative of wind turbine blade structures and compared different taper angles. The results showed that transition geometry could substantially influence both static strength and fatigue behavior. (sciencedirect.com)
The engineering lesson is:
Changing thickness is not only a dimensional change; the transition itself becomes part of the structural design.
Poorly designed thickness transitions can create:
- stress concentrations,
- local debonding,
- core cracking,
- premature fatigue damage.
21. Real Engineering Case — Marine Deck
Consider a conceptual marine deck panel.
Option A
80 kg/m³ × 20 mm
Option B
60 kg/m³ × 30 mm
Option B has a lower-density core but greater thickness.
If bending stiffness governs, the thicker sandwich may provide an attractive structural-to-weight ratio.
However, if the deck contains concentrated loads from:
- seats,
- machinery,
- fittings,
- supports,
local high-density reinforcement may still be required.
This illustrates the value of combining:
Low-density structural core + local high-density reinforcement.
22. Real Engineering Case — Transportation Floor
Transportation flooring experiences a combination of:
- distributed load,
- wheel load,
- point load,
- vibration,
- impact,
- fatigue.
A practical design may use:
Medium-density PVC Foam Core
for the main panel, combined with:
Higher-density inserts
under concentrated load locations.
Increasing the entire panel to a very high density may increase weight without providing equivalent benefit.
The engineering objective is:
Put material where the load requires it.
23. Core Thickness and Local Buckling
Core thickness can also influence face-sheet stability.
A sandwich core supports the face sheets against local instability.
If the core is too thin or too compliant, the face sheet can wrinkle under compression.
Potential solutions include:
- Increasing core thickness
- Increasing core density
- Increasing core shear modulus
- Increasing face-sheet thickness
- Improving bonding
The correct solution depends on which parameter is controlling the instability.
24. When Increasing Density Is Better Than Increasing Thickness
Increasing density may be preferable when:
1. Point loads dominate
The core needs greater compression strength.
2. Insert loads dominate
Fasteners or fittings require local load transfer.
3. Core shear governs
The existing core cannot support the required shear stress.
4. Geometry cannot accommodate additional thickness
The available envelope may be fixed.
5. Local reinforcement is required
A high-density patch can be more efficient than increasing the entire panel thickness.
25. When Increasing Thickness Is Better Than Increasing Density
Increasing thickness may be preferable when:
1. Bending stiffness governs
The panel needs greater structural depth.
2. Panel span is large
Long spans amplify deflection.
3. Weight reduction is critical
A lower-density but thicker core may produce high stiffness efficiently.
4. Global buckling is a concern
Greater sandwich depth can improve structural stability.
5. The face sheets already provide sufficient strength
The core mainly needs to separate and stabilize the skins.
26. Engineering Optimization Workflow
A practical design workflow can be:
Step 1 — Define Load
Determine:
- bending,
- shear,
- compression,
- point load,
- impact,
- fatigue.
↓
Step 2 — Identify Governing Failure Mode
Determine whether the design is controlled by:
- core shear,
- compression,
- buckling,
- indentation,
- face-sheet failure,
- interface failure.
↓
Step 3 — Select Preliminary Density
Choose a candidate PVC Foam Core grade.
↓
Step 4 — Select Thickness
Adjust thickness based on stiffness and geometry.
↓
Step 5 — Evaluate Weight
Calculate core mass.
↓
Step 6 — Evaluate Manufacturing
Check:
- machining,
- infusion,
- bonding,
- handling.
↓
Step 7 — Validate
Test the complete sandwich structure.
27. Testing Standards for Thickness-Density Optimization
| Property | Standard | Why It Matters |
|---|---|---|
| Density | ASTM C271/C271M | Confirms actual density |
| Thickness | ASTM C366/C366M | Dimensional verification |
| Core Shear | ASTM C273/C273M | Shear capacity/modulus |
| Core Compression | ASTM C365/C365M | Compression performance |
| Water Absorption | ASTM C272/C272M | Environmental conditioning |
| Sandwich Flexure | ASTM C393/C393M | Structural behavior |
| Facesheet Properties | ASTM D7249/D7249M | Skin contribution |
| Sandwich Stiffness | ASTM D7250/D7250M | Bending/shear stiffness |
| Flatwise Tensile | ASTM C297/C297M | Interface/core behavior |
| Dimensional Stability | ASTM D6772/D6772M | Environmental stability |
ASTM’s composite standards framework includes these core and sandwich test methods for material and structural characterization. (store.astm.org)
28. Why Complete Sandwich Testing Is Necessary
Suppose two PVC Foam Core grades have:
Similar Density
but different:
- shear modulus,
- cell morphology,
- surface quality,
- dimensional stability.
Their finished sandwich panels can behave differently.
Similarly, the same PVC Foam Core grade can behave differently when manufactured with:
- different face sheets,
- different resin systems,
- different adhesive thickness,
- different cure conditions,
- different machining.
Therefore:
[
\text{Core Qualification}
\neq
\text{Complete Sandwich Qualification}
]
Both are necessary for critical applications.
29. Manufacturing Effects on Thickness Selection
Increasing core thickness can introduce manufacturing challenges.
Potential issues include:
- longer infusion distance,
- more difficult conformability,
- increased handling damage,
- more complex edge treatment,
- greater machining depth,
- higher dimensional tolerance requirements.
For thick PVC Foam Core, suppliers should be able to control:
- thickness,
- flatness,
- density,
- machining depth,
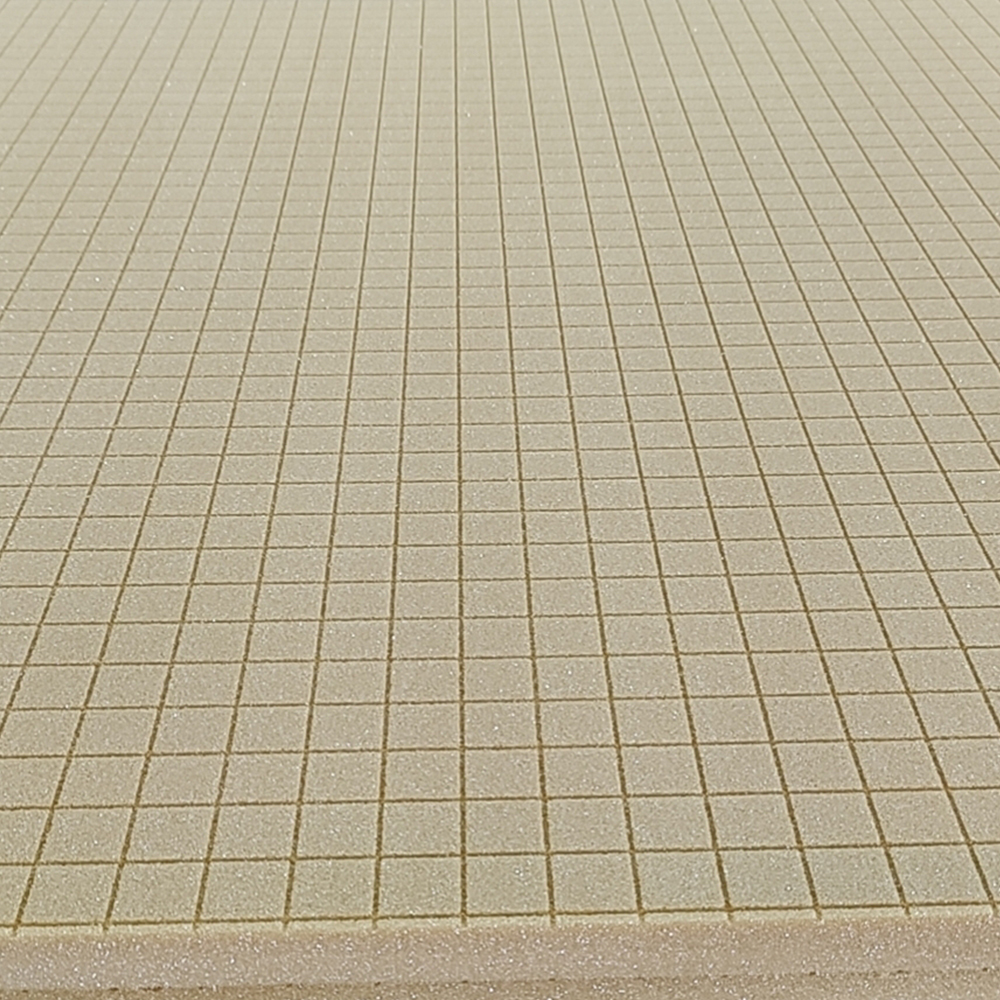
- groove geometry,
- taper accuracy.
A theoretical optimum that cannot be manufactured consistently is not a practical optimum.
30. Thickness Tolerance and Structural Performance
Consider a nominal:
30 mm PVC Foam Core
If actual thickness varies significantly across the panel, the sandwich depth also varies.
That can create:
- stiffness variation,
- local stress concentration,
- uneven face-sheet support,
- dimensional problems.
Therefore, procurement should define:
Nominal Thickness + Tolerance + Measurement Method
rather than simply:
30 mm Core
31. Density Tolerance Is Equally Important
Suppose the target density is:
80 kg/m³
The actual production material may vary around that target.
Density variation can affect:
- core weight,
- compression properties,
- shear properties,
- machining behavior,
- panel consistency.
For structural applications, the buyer should request:
- nominal density,
- allowable tolerance,
- batch-to-batch variation,
- sampling procedure,
- test method.
32. Supplier Comparison: A Better Procurement Table
Instead of comparing only price:
| Supplier | Density | Thickness | Price |
|---|---|---|---|
| A | 80 | 20 mm | Low |
| B | 80 | 20 mm | Medium |
| C | 80 | 20 mm | High |
Use:
| Parameter | Supplier A | Supplier B | Supplier C |
|---|---|---|---|
| Density Tolerance | |||
| Thickness Tolerance | |||
| Shear Strength | |||
| Shear Modulus | |||
| Compression Strength | |||
| Density Uniformity | |||
| Machining Accuracy | |||
| Taper Capability | |||
| Surface Quality | |||
| Test Documentation | |||
| Batch Traceability | |||
| Production Capacity | |||
| Sample Qualification |
This allows buyers to compare engineering value, rather than only purchase price.
33. Procurement Decision: Density or Thickness?
A buyer can use this simplified logic.
If the engineer says:
“Panel is too flexible.”
→ First investigate core thickness and sandwich depth.
If the engineer says:
“Core is crushing.”
→ Investigate core density/compression strength.
If the engineer says:
“Core is shearing.”
→ Investigate shear strength + thickness + load area.
If the engineer says:
“Face sheet is wrinkling.”
→ Investigate core modulus + thickness + skin design.
If the engineer says:
“Point load creates a dent.”
→ Investigate local high-density reinforcement.
If the engineer says:
“Panel is too heavy.”
→ Investigate lower-density core + increased thickness, where geometry permits.
34. A Practical Optimization Example
Suppose a conceptual panel requires:
- High bending stiffness
- Moderate shear load
- Low weight
- Several concentrated mounting points
A poor strategy would be:
High-density core throughout the panel
A potentially better strategy would be:
General Panel
60–80 kg/m³ PVC Foam Core
Structural Regions
80–100 kg/m³
Mounting Locations
120–200+ kg/m³ local reinforcement
Thickness
Increase the general core thickness to obtain the required bending stiffness.
This creates a hybrid density-thickness architecture.
35. Optimization Is a Multi-Objective Problem
The final design should balance:
[
\text{Minimize Mass}
]
subject to:
[
\text{Stiffness} \geq \text{Required}
]
[
\text{Strength} \geq \text{Required}
]
[
\text{Fatigue Life} \geq \text{Required}
]
[
\text{Manufacturability} \geq \text{Required}
]
[
\text{Safety Margin} \geq \text{Required}
]
This is a much more realistic engineering formulation than simply selecting the strongest core.
36. Procurement Should Follow the Structural Requirement
The buyer should not independently choose:
“We usually buy 80 kg/m³.”
Instead, the engineering department should provide:
- Required density range
- Required thickness
- Required mechanical properties
- Machining geometry
- Environmental requirements
- Test standards
- Tolerances
Procurement then evaluates suppliers against the approved technical specification.
This prevents purchasing decisions from driving structural design.
37. Recommended RFQ Format
A professional PVC Foam Core RFQ can be structured like this:
Product
PVC Foam Core Material
Application
Composite Sandwich Panel
Density
Target: ___ kg/m³
Tolerance: ___
Thickness
Target: ___ mm
Tolerance: ___
Mechanical Requirements
| Property | Minimum Requirement | Test Standard |
|---|---|---|
| Shear Strength | ___ | ASTM C273 |
| Shear Modulus | ___ | ASTM C273 |
| Compression Strength | ___ | ASTM C365 |
| Density | ___ | ASTM C271 |
| Water Absorption | ___ | ASTM C272 |
Machining
- Groove
- Perforation
- CNC contour
- Taper
- Custom cutting
Quality
- Batch traceability
- Inspection report
- Test report
- Dimensional inspection
38. Supplier Capability Checklist
Before approving a PVC Foam Core manufacturer, verify whether the supplier can provide:
- Multiple density grades
- Multiple thicknesses
- Consistent cell structure
- CNC machining
- Grooving
- Perforation
- Tapering
- Contour cutting
- Custom sheet dimensions
- Batch traceability
- Mechanical test reports
- Production samples
- Technical support
The ability to supply several density/thickness combinations is particularly valuable for engineering optimization.
39. Five Questions for a Technical Supplier
1. Can you supply the same PVC Foam Core in multiple densities?
This helps engineers optimize density zoning.
2. Can you provide multiple thicknesses?
This allows stiffness optimization.
3. Can you produce tapered or contoured core?
Important for complex composite structures.
4. Can you machine grooves and perforations according to engineering drawings?
Important for vacuum infusion and structural consistency.
5. Can you provide mechanical data for the actual production grade?
This is essential for qualification.
40. Final Engineering Decision Matrix
| Design Problem | Preferred First Investigation |
|---|---|
| Excessive Deflection | Increase Core Thickness |
| Core Shear Failure | Increase Shear Capacity |
| Local Crushing | Increase Density Locally |
| High Panel Weight | Reduce Density / Optimize Thickness |
| Buckling | Increase Sandwich Depth |
| Point Load Damage | Local Reinforcement |
| Poor Fatigue Life | Improve Complete Sandwich System |
| Interface Failure | Improve Bonding |
| Manufacturing Difficulty | Optimize Thickness/Machining |
| Excessive Cost | Optimize Density Zoning |
41. Final Design Checklist
Before freezing a PVC Foam Core specification, engineers should confirm:
Structural
- Governing load case identified
- Governing failure mode identified
- Required bending stiffness calculated
- Core shear verified
- Compression verified
- Buckling verified
- Local loads evaluated
- Fatigue evaluated where applicable
Material
- Density selected
- Thickness selected
- Mechanical properties verified
- Environmental properties evaluated
Manufacturing
- Machining validated
- Groove geometry confirmed
- Perforation confirmed
- Taper confirmed
- Bonding process validated
Procurement
- Tolerance specified
- Test standards specified
- Batch traceability required
- Supplier samples approved
- Production capacity confirmed
42. Conclusion: Optimize the Sandwich, Not Just the Core
The central engineering principle of PVC Foam Core selection can be summarized in one sentence:
Density determines much of the core’s intrinsic mechanical capability, while thickness creates structural leverage through face-sheet separation.
Neither variable should be optimized independently.
For bending-dominated structures, increasing core thickness can be an extremely effective way to increase stiffness without simply increasing core density.
For concentrated loads and compression-dominated regions, higher-density PVC Foam Core may be more appropriate.
For complex structures, the most efficient solution may be a combination of:
Density Zoning
Thickness Zoning
Local Reinforcement
Controlled Machining
Qualified Face-Sheet/Core Bonding
This approach is particularly valuable in wind turbine blades, marine structures, transportation panels and large industrial sandwich structures, where every additional kilogram can have a downstream effect on structural design, handling and operating efficiency.
The engineering process should therefore move through:
Load Analysis
→ Failure Mode Identification
→ Density Selection
→ Thickness Optimization
→ Manufacturing Validation
→ Sandwich Testing
→ Structural Qualification
→ Production Control
For procurement teams, the implication is equally important.
Do not ask only:
“What is your PVC Foam Core price per cubic meter?”
Ask:
“Which density and thickness combinations can you supply consistently, what mechanical data support them, what machining tolerances can you control, and can you provide qualified production samples?”
That is the difference between purchasing a foam material and sourcing a structurally qualified composite core system.
